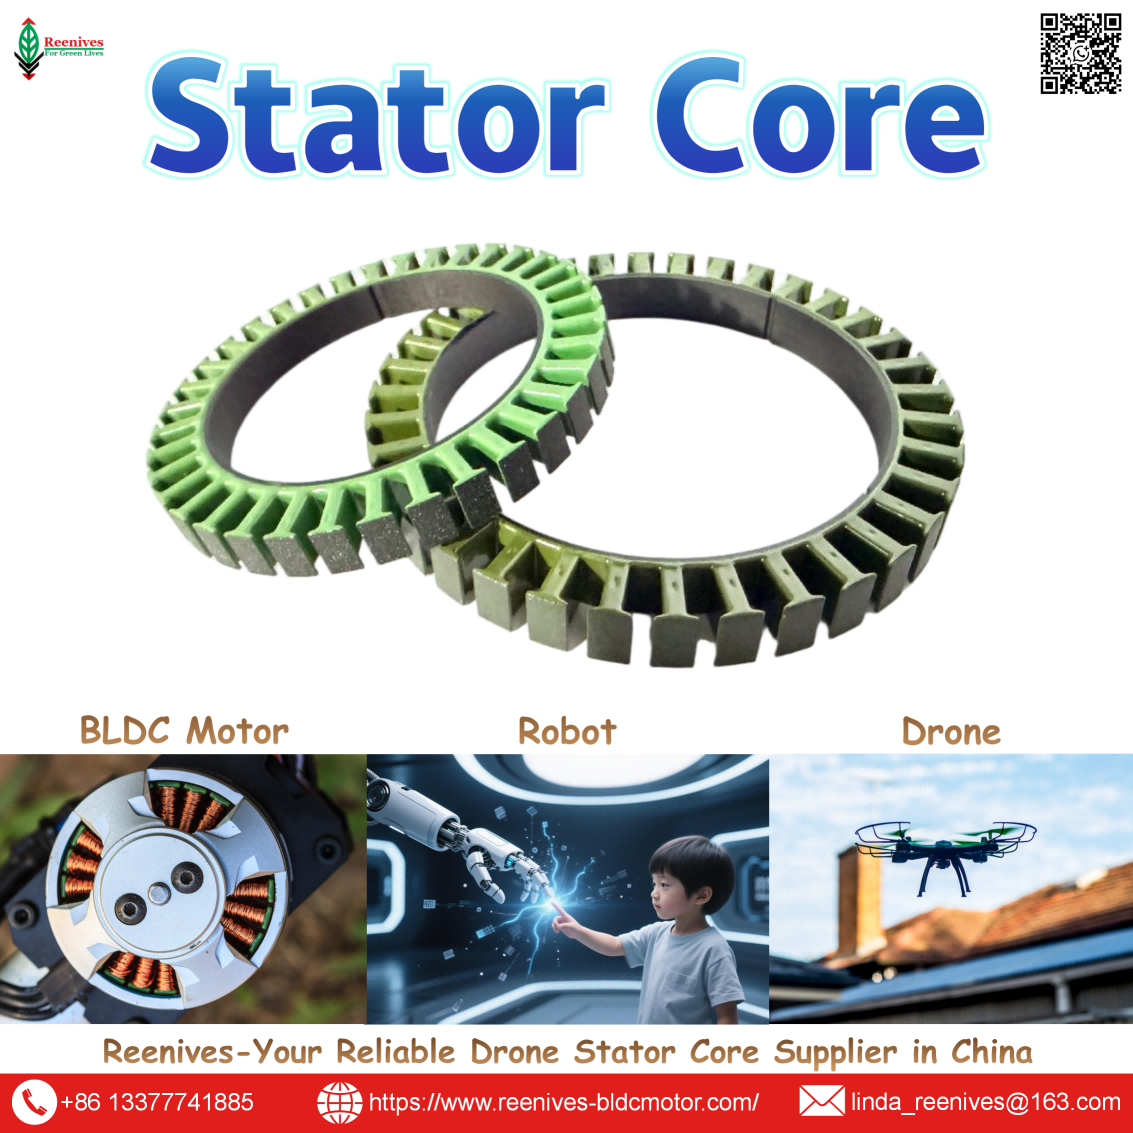
Reenives: Global Leading BLDC Drone Motor Stator Winding Service Supplier

BLDC Drone Motor Stator Winding Service: The Four Scope Tiers That Decide Who Owns the Failure
“We can wind that for you” is not a scope. It is an opening sentence. Two winding service quotations can both sound competent and differ enormously in what the supplier actually owns. One winds the customer’s stator cores and returns them; the other supplies the cores, winds them, tests every unit, and delivers a matched stator-rotor pair with a traceability record. When a stator fails a surge test three months later, the first supplier says the core was out of tolerance, the customer says the winding damaged the enamel, and the dispute is unresolvable because the scope never said who was responsible for the interface. The winding itself was never the problem.
The published parameters show how much sits inside that interface. A drone stator winding process must hold ±0.05 N tension and ±0.03 mm placement accuracy, on 0.18–0.25 mm wire, and reach a slot fill of 30–40% for manual or low-tier winding versus 75% with advanced multi-axis CNC layered patterns. But the winding cannot escape the core: a 0.20 mm lamination grade at ≤8.5 W/kg at 1.0 T / 400 Hz, stacking factor ≥97.5%, burr height <0.03 mm, and ±0.05 mm critical tolerance together set whether the winder can enter the slot, survive the tension, and seat the stator consistently. Whichever party owns the core owns half the winding outcome — and a winding service that does not supply the core has not accepted that half.
This guide is written for the procurement engineer or process lead deciding what to outsource and what to keep in-house. It defines the four winding service tiers by scope, separates the core parameters from the winding parameters, presents the published process and test data with their standards, maps the tiers to drone, UAV, and FPV mission profiles, and closes with a five-step supplier audit that starts with the scope boundary rather than the price.
In this guide — jump to the section your project needs:
- What Is a Stator Winding Service? The Scope Boundary Defined
- Four Service Tiers: Labor Only, Core + Winding, Wound + Tested, and Matched Pair
- Published Parameters: Core Specs, Tension, Placement, Slot Fill, and 100% Test Coverage
- Application Profiles: Which Service Tier Fits Which Drone, UAV, and FPV Mission
- A 5-Step Winding Service Supplier Audit
- FAQ: Scope, Tension, Core Ownership, Test Coverage, Slot Fill, and Quotation Contents
- Summary: Buy the Scope, Then the Winding
What Is a Stator Winding Service? The Scope Boundary Defined
A stator winding service is a manufacturing service that inserts enameled copper wire into stator slots in a defined pattern, terminates the phase leads, and — depending on the agreed scope — supplies the stator core, performs electrical verification, and may include the matched rotor. The service is defined not by the machine it runs but by where its responsibility stops.
| Activity | Why It Belongs in the Scope Discussion | Consequence If Unassigned |
|---|---|---|
| Stator core supply | Slot geometry, coating condition, burr, and tolerance determine whether the winding can be executed without damage | Core-induced winding defects become an unresolvable dispute between core supplier and winder |
| Winding execution | Tension, placement, turns, and pattern determine Kv, phase balance, and short risk | The customer has no verifiable record of the process that produced the stator |
| Electrical test | Hi-Pot, three-phase resistance, and surge waveform detect defects the winding and core may both have contributed to | Latent turn-to-turn shorts pass into assembly and fail in the field |
| Matched rotor | The air gap is created by stator bore and rotor OD together, not by either alone | Vibration and bearing failures are attributed to the motor design rather than to the pair mismatch |
Sources: Reenives stator core specification (slot geometry, coating, burr, tolerance); published winding process parameters (tension, placement); JYSTATOR drone stator winding specification (100% Hi-Pot, 3-phase resistance, surge waveform).
The reason the scope boundary matters more than the per-unit price is that a winding service cannot own a failure mode that originates outside its scope. If the customer supplies the core and the core has a burr that pierces the coating during winding, the resulting turn-to-turn short is a joint failure — but only one party was ever in a position to prevent it. When the same supplier produces the core, winds it, and tests it, that ambiguity disappears: the supplier owns the interface, and the customer's incoming inspection becomes a verification rather than a forensic exercise.
Procurement translation: before comparing two winding service quotations, write the scope boundary in one sentence. “Customer supplies 12N14P 0.20 mm cores; supplier winds to 12 turns/phase on 0.20 mm wire and returns untested” is a Tier 1 scope. “Supplier supplies 0.20 mm cores at ≤8.5 W/kg, winds to specification, and delivers 100% Hi-Pot / 3-phase resistance / surge-tested stators with batch records” is a Tier 3 scope. The two quotes are not competitors; they are different products.
Four Service Tiers: Labor Only, Core + Winding, Wound + Tested, and Matched Pair
Tier 1 — Labor-only winding
The customer supplies the stator cores, the wire, the turn count, and the winding pattern. The service inserts the wire and terminates the leads. This tier suits buyers who already control core supply and want to use a specialist winder for capacity or for a specific fine-wire capability they do not have in-house. Its limitation is structural: the service cannot own core defects, because it did not make the core and cannot reject a customer-supplied part without delaying the order. Slot geometry that is too tight, coating that is thin at the slot edge, or burr that exceeds the coating thickness will all become winding defects that the service will attribute to the core.
Tier 2 — Core plus winding
The service supplies the stator core and performs the winding. This is the tier where the core specification becomes part of the deliverable, and it is the tier that most drone motor programmes should be comparing against when they evaluate a winding quotation. The published core parameters that belong in this scope are 0.20 mm silicon steel, core loss ≤8.5 W/kg at 1.0 T / 400 Hz, stacking factor ≥97.5%, burr height <0.03 mm, critical tolerance ±0.05 mm, and uniform epoxy coating. With those named, the service owns both the physical boundary the winding works within and the winding execution itself. What it does not necessarily own is the evidence that the finished winding stator is electrically sound.
Tier 3 — Wound and tested
The service supplies the core, winds it, and performs 100% electrical testing on every unit: Hi-Pot for insulation integrity, three-phase resistance by four-wire measurement at ±0.5% tolerance for winding consistency, and surge waveform testing for turn-to-turn short circuits. Broader frameworks add insulation resistance, phase balance, and polarity checks. This tier is the minimum for a drone programme where a latent short would reach a flight controller, because surge testing is the only standard test that detects a turn-to-turn defect that leaves total phase resistance within tolerance. What Tier 3 does not cover is the air gap — the rotor is still the customer's part.
Tier 4 — Matched stator-rotor pair
The service supplies the wound and tested stator, the rotor with its magnets, and controls the pair-level dimensions: air-gap geometry, concentricity between stator bore and rotor outer diameter, thermal-expansion allowance between the stator stack and the rotor bell, and batch traceability linking a magnet batch to a lamination batch. This is the tier that owns the full failure chain. It is not necessary for every programme — a customer with an in-house rotor line and an established pair-matching process can work at Tier 3 — but for a programme that is scaling from prototype to volume and has experienced unexplained vibration or KV drift, the pair-level scope is usually the missing control.
| Tier | Supplier Supplies | Supplier Owns | Best Fit |
|---|---|---|---|
| 1 · Labor only | Winding execution | Winding process only | Buyers with in-house core supply and a specific capacity gap |
| 2 · Core + winding | Core and winding | Core-induced and winding-induced defects | Most drone and UAV programmes evaluating a winding quotation |
| 3 · Wound + tested | Core, winding, 100% electrical test | Plus latent short detection and test records | Programmes where a field failure is costly — FPV, inspection, agricultural |
| 4 · Matched pair | Core, winding, test, rotor | Plus air gap, concentricity, thermal allowance, traceability | Programmes scaling to volume or recovering from unexplained vibration or KV drift |
Published Parameters: Core Specs, Tension, Placement, Slot Fill, and 100% Test Coverage
Core parameters — the boundary the winding works within
A winding service that supplies cores must publish the core specification, not just the lamination thickness. Reenives publishes its drone stator cores at 0.20 mm silicon steel, core loss ≤8.5 W/kg at 1.0 T / 400 Hz, stacking factor ≥97.5%, burr height <0.03 mm, critical tolerance ±0.05 mm, concentricity ≤0.02 mm, and uniform epoxy coating, in slot/pole configurations including 9N12P, 12N14P, 18N24P, and 24N28P. Each of those values maps to a winding consequence: core loss sets the thermal budget the winding must not exceed; stacking factor determines the flux density the copper can link; burr height determines whether the coating survives wire insertion; tolerance determines whether the stator seats consistently in the winding fixture; concentricity determines the air gap the wound stator will operate across.
Winding parameters — tension, placement, wire, pattern
Published winding process data places tension fluctuation within ±0.05 N and wire placement accuracy better than ±0.03 mm. Drone-specific equipment uses a precision tension controller at ±5 g. The wire range for a 12N14P drone stator is 0.18–0.25 mm single strand or 3×0.12–4×0.13 mm parallel, and a KV900 rating corresponds to approximately 12 turns per phase (4 turns per slot × 3 slots per phase). The winding pattern for 12N14P is typically ABCABCABCABC, with direction documented tooth by tooth — a single reversed tooth produces a phase imbalance the ESC interprets as a desync condition.
Slot fill — the copper density metric and its ceiling
Published slot fill ranges from roughly 30–40% for manual or low-tier machine winding to 75% for advanced multi-axis CNC with layered or interleaved patterns, with one supplier reporting 80% using electronic cam non-linear linkage control. The ceiling is set by the core: typically the winding space must leave at least three times the wire diameter for the needle or flyer to enter, so a slot opening designed to reduce cogging limits the achievable fill. Higher fill increases the torque constant and reduces line-to-line resistance without changing the motor’s physical footprint — which is why the fill target belongs in the quotation and should be verified on a sample rather than assumed from the machine’s brochure.
Test coverage — the evidence that the scope was closed
Published drone stator test specifications call for 100% electrical performance testing on every wound stator, covering Hi-Pot, three-phase resistance, and surge waveform testing, with four-wire resistance measurement to ±0.5% tolerance. The surge test is the differentiator: a turn-to-turn short can leave total phase resistance within tolerance while generating a hot spot under load, so a resistance-only check passes the defect. A winding service that samples these tests rather than performing them on every unit is managing the process average, not the shipment.
The tier-1 dispute that repeats: a customer supplies cores with a burr at the upper edge of its own tolerance band. The winding service inserts the wire, the burr abrades the enamel, and the stator fails surge testing. The service says the core was out of specification; the customer says the service should have detected it. Neither party is wrong, and neither can resolve it — because the scope did not assign the interface. The only structural fixes are to move to Tier 2 (the service supplies the core), to add an incoming core inspection with a stated burr and coating acceptance criterion, or to accept the risk explicitly in the purchase order.
Application Profiles: Which Service Tier Fits Which Drone, UAV, and FPV Mission
| Mission Class | Recommended Tier | Why | Key Specification to Name |
|---|---|---|---|
| FPV racing / high-RPM | Tier 3 (wound + tested) | Fine wire at high electrical frequency makes latent shorts both more likely and more costly | 100% surge testing; tension ±0.05 N; core loss ≤8.5 W/kg @ 1.0 T / 400 Hz |
| Cinematic / inspection FPV | Tier 3, moving to Tier 4 | Vibration reaches the payload before it reaches the motor; air-gap control becomes visible | Concentricity ≤0.02 mm; 3-phase resistance balance; matched pair once volume justifies it |
| Agricultural spraying UAV | Tier 4 (matched pair) | Continuous duty, wet environment, and heavy current demand a single owner for the full failure chain | Uniform epoxy coating; matched stator-rotor with hot-state air-gap allowance |
| Heavy-lift / logistics UAV | Tier 4 | Long service life makes stacking factor and magnet grade a total-cost-of-ownership issue | Stacking ≥97.5%; N42SH-class magnets; batch traceability across the pair |
| Prototype / low-volume validation | Tier 2 or 3 | Volume does not yet justify pair-level control, but latent shorts still waste validation cycles | Core + winding + 100% test; sample-first workflow |
The pattern is that the recommended tier rises with the cost of a field failure. FPV and cinematic programmes can operate at Tier 3 because the stator is the dominant winding risk and the rotor is a known quantity. Agricultural and heavy-lift programmes generally move to Tier 4 because the duty cycle is long, the environment is hostile, and the cost of an in-flight failure is high enough that a single owner for the full chain is cheaper than the ambiguity. Prototype programmes sit at Tier 2 or 3 because the priority is validation speed, not lifetime cost.
A 5-Step Winding Service Supplier Audit
- Write the scope boundary before requesting a price. State which of the four activities the service covers: core supply, winding, electrical test, and matched rotor. A quotation that arrives without a scope statement is not comparable to one that includes it — and the cheapest quote is usually the narrowest scope. If the service cannot state its tier, ask which party is expected to resolve a turn-to-turn short caused by a core burr.
- If the service supplies the core, require the full core parameter set — not just the lamination thickness. Name 0.20 mm silicon steel, core loss ≤8.5 W/kg at 1.0 T / 400 Hz per IEC 60404-2, stacking factor ≥97.5%, burr height <0.03 mm, critical tolerance ±0.05 mm, concentricity ≤0.02 mm, and uniform epoxy coating. A service that quotes “0.20 mm steel” without these values is working inside a boundary it has not defined, and any core-induced defect will surface as a winding failure.
- Require the tension window and placement accuracy as process parameters. Ask for ±0.05 N tension fluctuation and ±0.03 mm placement accuracy, and request the tension controller resolution (±5 g) and a fluctuation test report. These are the parameters that determine whether the enamel survives, and they are not visible in a finished stator inspection.
- Confirm the electrical test list and the coverage — then ask for a rejected unit. Specify 100% Hi-Pot, three-phase resistance (four-wire, ±0.5%), and surge waveform testing. Ask for a recent record showing a stator that failed surge testing and was rejected. A service with no rejected units is either perfect or not testing, and the surge test is the only one that detects a turn-to-turn short that resistance measurement passes.
- Run a trial wind with production cores and production wire, and review the fill result. Send two to three cores and the exact wire specification, have the service wind the sample, and inspect wire lay, slot fill, enamel condition at the slot edges, and the electrical test output. Ask for the achieved fill factor, not the machine’s theoretical maximum. Only after the sample passes should price, volume band, and lead time be negotiated.
FAQ: Scope, Tension, Core Ownership, Test Coverage, Slot Fill, and Quotation Contents
What does a drone motor stator winding service actually include?
A winding service can include any subset of four activities: inserting enameled copper wire into stator slots in a defined pattern, terminating the phase leads, performing electrical tests (Hi-Pot, three-phase resistance, surge waveform), and supplying the stator core itself as part of the deliverable. The scope boundary is the single most important line in the quotation, because it determines which failure modes the supplier owns. A labor-only service owns winding defects but not core defects; a wound-and-tested service owns both the winding and the electrical verification; a matched stator-rotor service also owns the air-gap geometry. Published drone stator winding specifications call for 100% coverage of Hi-Pot, three-phase resistance, and surge waveform testing on every wound stator, which is the minimum evidence that the winding scope was actually closed.
Source: JYSTATOR drone stator winding specification (100% Hi-Pot, 3-phase resistance, surge waveform); Reenives scope-tier framework.
What tension and wire placement accuracy should a winding service hold for drone stators?
Published winding process data places tension fluctuation within ±0.05 N and wire placement accuracy better than ±0.03 mm. Drone-specific equipment uses a precision tension controller at ±5 g to prevent breakage of fine wire and over-stretching. The window is narrow because drone stator wire runs 0.18–0.25 mm single strand or 3×0.12–4×0.13 mm parallel, and the enamel coating is only micrometres thick. Excessive tension stretches and thins the enamel, creating a turn-to-turn short risk that may not appear until the motor has flown for hours; insufficient tension leaves a loose coil that reduces slot fill factor and vibrates under flight loads. A winding service that cannot state its tension window and placement accuracy has not described its process.
Source: Published winding process data (±0.05 N fluctuation; ±0.03 mm placement; ±5 g tension controller; 0.18–0.25 mm wire).
Why does the stator core need to be part of the winding service scope?
Because the core sets the physical boundary the winding must work within, and a core defect becomes a winding defect. Slot opening geometry determines whether an automated flyer or needle can enter and how much copper can be packed in — typically three times the wire diameter of entry clearance is required. Insulation coating integrity determines how much tension the enamel can survive. Burr height on lamination edges can pierce the coating during winding and create a latent short. Dimensional tolerance controls how consistently the stator seats in the winding fixture. When the customer supplies the core and the service only winds it, any of those core-side conditions becomes a dispute about who caused the failure. When the service supplies both, the accountability is single-source.
Source: Published winding process constraints (slot opening, coating integrity, burr effect); Reenives stator core specification.
What electrical tests should a winding service perform and at what coverage?
Published drone stator test specifications call for 100% electrical performance testing on every wound stator, covering Hi-Pot for insulation integrity, three-phase resistance for winding consistency, and surge waveform testing for turn-to-turn short circuits. Broader frameworks add insulation resistance, phase balance, and polarity or rotation checks. Surge testing is the critical differentiator because a turn-to-turn short can leave total phase resistance within tolerance while creating a hot spot under load, so a resistance-only check passes the defect. Four-wire resistance measurement is used for accuracy, with typical tolerance around ±0.5%. A winding service that samples these tests rather than performing them on 100% of units is managing the average, not the shipment.
Source: JYSTATOR drone stator winding specification (100% coverage; four-wire measurement to ±0.5%); published stator test framework.
What slot fill factor can a winding service realistically achieve on a drone stator?
Published ranges are wide. Traditional manual or low-tier machine winding yields roughly 30% to 40% copper slot fill because of unorganized wire crossovers and air gaps. Advanced multi-axis CNC winding with layered or interleaved patterns reaches 75%, and one supplier reports 80% using electronic cam non-linear linkage control. The achievable value depends on the stator core’s slot opening geometry as much as on the winding equipment: a small slot opening designed to reduce cogging limits how much copper can be inserted. Higher fill factor increases the torque constant and reduces line-to-line resistance without changing the motor’s physical footprint, which is why the fill target should be specified and verified on a sample rather than assumed.
Source: Published drone winding selection guide (30–40% manual; CNC layered patterns); Nuoyuan winding analysis (75–80%; three-times wire diameter entry clearance).
What should a winding service quotation contain to be comparable?
A comparable quotation names the scope boundary (labor only, core plus winding, wound and tested, or matched pair), the stator core specification if the service supplies it (lamination grade and thickness, core loss at a defined test point per IEC 60404-2, stacking factor, burr height, tolerance, coating), the winding parameters (wire diameter, strand count, turns per phase, winding pattern, tension window, placement accuracy, slot fill target), the electrical test list and coverage, the sample and first-article process, the volume band and lead time, and the tooling or fixture cost if any. A quote that names only a per-unit winding price and a wire gauge is not comparable to one that names all of the above.
Source: Reenives winding service quotation framework; published winding process and test parameters.
Summary: Buy the Scope, Then the Winding
A stator winding service is defined by where its responsibility stops, not by the machine it runs. The four tiers — labor only, core plus winding, wound and tested, and matched stator-rotor pair — transfer progressively more failure modes to the supplier, and the price difference between them is usually scope rather than margin. A quotation that names a per-unit winding price without naming its tier cannot be compared with one that does.
The published parameters define what a credible Tier 2+ scope contains. On the core side: 0.20 mm silicon steel, core loss ≤8.5 W/kg at 1.0 T / 400 Hz, stacking factor ≥97.5%, burr height <0.03 mm, critical tolerance ±0.05 mm, concentricity ≤0.02 mm, and uniform epoxy coating. On the winding side: ±0.05 N tension, ±0.03 mm placement accuracy, 0.18–0.25 mm wire, ≈12 turns per phase for KV900, ABCABCABCABC pattern, and a slot fill target verified on a sample. On the test side: 100% coverage of Hi-Pot, three-phase resistance by four-wire measurement, and surge waveform testing.
The audit takeaway is that the surge test record and the rejected unit are the two pieces of evidence that distinguish a winding service from a winding vendor. A service that performs 100% surge testing, can show a rejected stator, and can trace the test data to a batch is managing the scope it accepted. A service that quotes a wire gauge and a turn count has described the winding and left the core, the enamel damage, and the latent short with the buyer.
Outsourcing BLDC drone, UAV, or FPV stator winding?
Reenives supplies 0.20 mm silicon steel stator cores at core loss ≤8.5 W/kg at 1.0 T / 400 Hz per IEC 60404-2, stacking factor ≥97.5%, burr height <0.03 mm, critical tolerance ±0.05 mm, concentricity ≤0.02 mm, and uniform epoxy coating, in 9N12P, 12N14P, 18N24P, and 24N28P configurations — plus matched stator-rotor pairs, 100% electrical test records, private mould development, and free samples for qualified engineering evaluations.
WhatsApp: +86-13377741885
Email: linda_reenives@163.com
Official website: www.reenives-bldcmotor.com
Dongguan Runlu Motor Technology Co., Ltd.
Reenives — Drone Motor One-Stop Solution Supplier
Reenives is a professional drone stator core manufacturer, founded in 2022. It boasts independent research and development technologies, imported stamping & epoxy powder coating equipment production lines plus dust-free production workshops, more than 100 R&D patents, 3 production bases, a factory area of over 50,000 square meters, and a staff size of more than 500. From production to sales, we support bulk purchasing, private mould development, and sample making, and can provide tailor-made perfect solutions for your production and usage scenarios. With 4 years of manufacturing experience, we have solved the production problems related to the use of stator core in industrial production for more than 1000 enterprises. We can ship globally (with complete export qualifications). Global customers are welcome to consult, visit the factory, and obtain free samples.
0.20 mm silicon steelCore loss ≤8.5 W/kg @ 1.0 T / 400 HzStacking factor ≥97.5%Burr <0.03 mmConcentricity ≤0.02 mmMatched stator-rotor pairs100% test recordsGlobal export qualifications
Drone Motor Winding Stator Parameters Explanation
Related Article