
How to Produce BLDC Motor Iron Core
author: Zove
2025-05-23
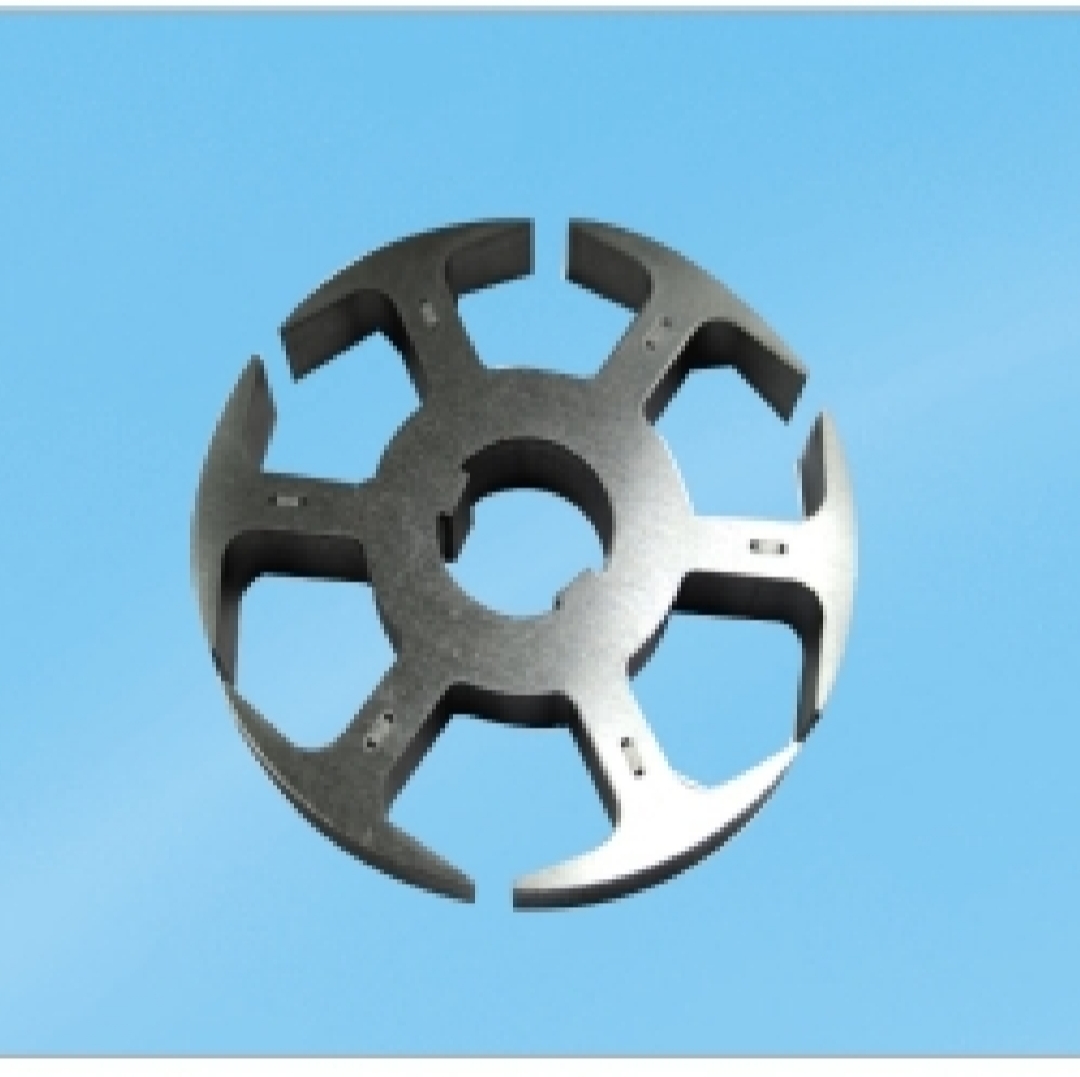
Below is a step-by-step overview of how iron cores are typically manufactured:
---
### **1. Material Selection**
- **Core Material**: High-grade **silicon steel (electrical steel)** is the most common choice due to its:
- Low hysteresis losses.
- High magnetic permeability.
- Thin, insulated laminations to reduce eddy currents.
- **Lamination Thickness**: Typically ranges from **0.1 mm to 0.5 mm**, depending on the motor’s operating frequency and power requirements.
---
### **2. Design and Simulation**
- **Electromagnetic Design**: Use Finite Element Analysis (FEA) software to optimize:
- Slot and pole configuration.
- Flux distribution.
- Torque ripple and cogging reduction.
- **Mechanical Design**: Define the geometry of laminations (slots, teeth, back iron) and ensure structural rigidity.
- **Electromagnetic Design**: Use Finite Element Analysis (FEA) software to optimize:
- Slot and pole configuration.
- Flux distribution.
- Torque ripple and cogging reduction.
- **Mechanical Design**: Define the geometry of laminations (slots, teeth, back iron) and ensure structural rigidity.
---
### **3. Manufacturing Process**
#### **Step 1: Stamping/Punching Laminations**
- **Process**: Thin silicon steel sheets are fed into a **progressive die stamping machine** to punch out the lamination profiles.
- Shapes include slots, teeth, and mounting holes.
- Precision tolerances (e.g., ±0.02 mm) are critical to avoid misalignment.
- **Lamination Coating**: Each lamination is coated with an insulating layer (e.g., phosphate, varnish, or oxide) to block eddy currents between layers.
#### **Step 2: Stacking and Bonding**
- **Stacking**: Laminations are stacked to form the stator or rotor core.
- Alignment is maintained using alignment pins or interlocking features.
- Stack height depends on the motor’s power and torque requirements.
- **Bonding Methods**:
- **Welding**: Spot welding at the edges (less common due to potential short-circuiting).
- **Adhesives**: Epoxy or glue applied between laminations.
- **Riveting**: Mechanical fasteners (rare in high-frequency applications due to eddy currents).
- **Self-bonding**: Laminations with adhesive coatings are heat-pressed.
#### **Step 3: Heat Treatment (Optional)**
- **Stress Relief Annealing**: Some cores undergo annealing to relieve internal stresses from stamping, improving magnetic properties.
- **Stress Relief Annealing**: Some cores undergo annealing to relieve internal stresses from stamping, improving magnetic properties.
#### **Step 4: Slot Insulation**
- **Insulating Liners**: Non-conductive materials (e.g., Nomex, polyester film) are inserted into stator slots to prevent winding shorts.
- **Insulating Liners**: Non-conductive materials (e.g., Nomex, polyester film) are inserted into stator slots to prevent winding shorts.
#### **Step 5: Winding Integration**
- **Copper Windings**: Coils are wound into the stator slots (for stator cores) using automated winding machines.
- **Vacuum Pressure Impregnation (VPI)**: The core is impregnated with resin to secure windings and improve thermal conductivity.
- **Copper Windings**: Coils are wound into the stator slots (for stator cores) using automated winding machines.
- **Vacuum Pressure Impregnation (VPI)**: The core is impregnated with resin to secure windings and improve thermal conductivity.
#### **Step 6: Rotor Core Assembly (if applicable)**
- **Permanent Magnet Mounting**: For rotor cores, magnets are glued or embedded into the laminated structure.
- **Balancing**: Dynamic balancing ensures smooth rotation at high speeds.
- **Permanent Magnet Mounting**: For rotor cores, magnets are glued or embedded into the laminated structure.
- **Balancing**: Dynamic balancing ensures smooth rotation at high speeds.
---
### **4. Quality Control**
- **Core Loss Testing**: Measure hysteresis and eddy current losses using a **Epstein frame** or **single-sheet tester**.
- **Dimensional Inspection**: Verify slot geometry, stack height, and concentricity with CMM (Coordinate Measuring Machine).
- **Magnetic Flux Testing**: Use a Gauss meter or flux mapper to ensure uniform flux distribution.
- **Electrical Tests**: Check insulation resistance between laminations.
---
### **Advanced Techniques**
1. **Laser Cutting**: For ultra-thin laminations (<0.1 mm) or complex geometries (e.g., hairpin stator slots).
2. **Additive Manufacturing**: 3D-printed soft magnetic composites (SMCs) for custom core shapes (emerging technology).
3. **Powder Cores**: Iron powder cores for high-frequency applications (rare in BLDC motors).
---
### **Key Challenges**
- **Minimizing Core Losses**: Balancing lamination thickness, material grade, and insulation.
- **Precision**: Tight tolerances for slot alignment and stack consistency.
- **Cost Optimization**: Reducing scrap material in stamping processes.
- **Minimizing Core Losses**: Balancing lamination thickness, material grade, and insulation.
- **Precision**: Tight tolerances for slot alignment and stack consistency.
- **Cost Optimization**: Reducing scrap material in stamping processes.
---
### **Applications of Finished Iron Cores**
- **Stator Cores**: Hold windings and guide flux in the stationary part of the motor.
- **Rotor Cores**: Support permanent magnets or electromagnets in the rotating part.
- **Stator Cores**: Hold windings and guide flux in the stationary part of the motor.
- **Rotor Cores**: Support permanent magnets or electromagnets in the rotating part.
---
### **Summary**
Producing a BLDC motor iron core requires advanced materials (silicon steel laminations), precision stamping and stacking, and rigorous quality control. The process balances **magnetic efficiency**, **mechanical strength**, and **cost** to meet the demands of high-performance motors used in EVs, robotics, and industrial automation.
Producing a BLDC motor iron core requires advanced materials (silicon steel laminations), precision stamping and stacking, and rigorous quality control. The process balances **magnetic efficiency**, **mechanical strength**, and **cost** to meet the demands of high-performance motors used in EVs, robotics, and industrial automation.
What is Rotor In a BLDC Motor
Why Iron Core is important for BLDC Motor
Related Article
Engineers and procurement teams routinely treat the stator as one line item inside a Drone Motor BOM, but the relationship between stator and motor is not a parts-list relationship — the stator sets the motor’s torque ceiling, its thermal limit, and its vibration signature before a single rotor magnet is installed.
What is Relationship Between Stator and Motor in Drone?

This guide answers What is a PCB Stator Motor? at the level a procurement engineer or propulsion lead needs: the physical definition, the three board architectures in production, the parameters that are actually measurable, the UAV mission profiles where the trade is favorable, and the five-step workflow for deciding whether to specify one.
What is PCB Stator Motor?

If your drone motor sags at minute ten or your robot joint trips on overcurrent, the component count did not cause it. A brushless Drone Motor can be broken down into a tidy list of functional assemblies, and that list will not tell you why one propulsion unit holds thrust through a full agricultural spray cycle while another loses it under thermal load.
How Many Components Included in a Drone Motor?
A drone motor that loses thrust after eight minutes of hover, or fails a production hipot test after passing a bench run, is rarely failing because the magnets were weak or the ESC was undersized. It is failing because the generator stator winding assumptions baked into the specification were never valid for a UAV BLDC stator. In a conventional generator, the stator carries the armature winding — the winding in which voltage is induced — and the field is on the rotor or on salient poles.
What is Generator Stator Winding?