BLDC Drone Motor Stator Rotor Stamping Supplier

Rotor Stamping — Precision Stamping for BLDC Drone Motor Stators & Rotors | Reenives Stator Core Supplier
⚠️ Is your rotor stamping suffering from excessive burrs, short die life, or inconsistent tolerances? Poor stamping quality — worn dies, incorrect clearance, or inconsistent material feed — can increase core loss, cause stacking problems, and drive up production costs, especially in high-volume BLDC drone motor manufacturing where stator and rotor must be perfectly matched.
✅ Reenives provides high-precision rotor stamping and stator stamping engineered for BLDC drone motors. With imported high-speed progressive die stamping lines, precision carbide tooling, epoxy powder coating, and dust-free workshops, we deliver stamped stator and rotor cores with low burrs, tight tolerances, and long die life. As a reliable BLDC drone motor stator rotor stamping supplier, we help 1000+ enterprises improve motor reliability and reduce production costs.
📋 Table of Contents
What Is Rotor Stamping?
Rotor stamping is the process of cutting thin electrical steel sheets into precise rotor core shapes using a stamping press and hardened steel dies. The stamped laminations are then stacked, interlocked or bonded, and coated to form the rotor core of a motor. Each lamination is coated with a thin insulation layer to limit eddy currents between layers. The same stamping process is used to produce stator laminations.
In BLDC drone motors, rotor and stator stamping is the most common and cost-effective production method for high volumes. The stamping process directly determines:
- Dimensional accuracy & stacking factor
- Burr height & inter-lamination shorts
- Core loss & motor efficiency
- Rotor balance & bearing life
High-speed progressive die stamping with precision carbide tooling ensures consistent lamination geometry, minimal burrs, and long tool life — critical for high-volume BLDC drone motor production.

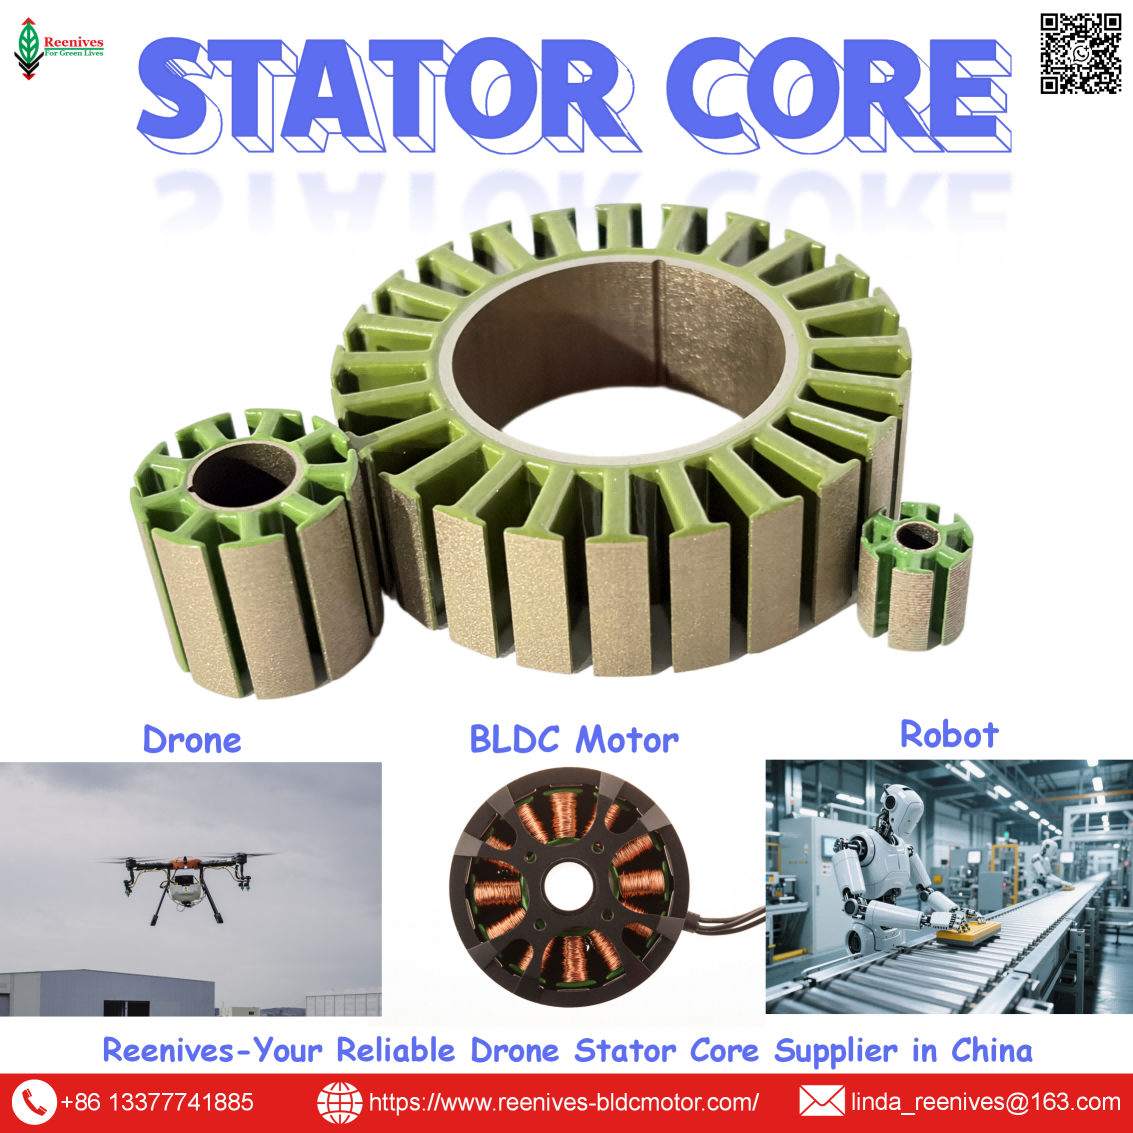
Precision rotor and stator stamping — manufactured by Reenives with imported high-speed stamping & epoxy powder coating lines.
Types of Rotor & Stator Stamping
Rotor and stator stamping can be performed using several methods, each suited to different production volumes, precision requirements, and cost targets. Reenives offers the following:
- High-Speed Progressive Die Stamping — Continuous coil feeding through a multi-station die. Highest efficiency for high-volume BLDC drone motor production. Low cost per piece, excellent consistency.
- Compound Die Stamping — Single-stroke die that cuts the entire lamination profile in one hit. Good for medium volumes, high precision.
- Segmented Stator Stamping — Individual teeth stamped separately for separate winding, then assembled into a full core. Higher slot fill factor.
- Rotor Stamping with Magnet Pockets — Rotor laminations stamped with interior magnet slots for IPM designs.
- Interlocked Stamping Stacks — Stamped laminations with integral dimples or dovetails for mechanical assembly. Cost-effective for high volume.
- Bonded Stamping Stacks — Stamped laminations bonded with adhesive instead of interlocking, reducing eddy current losses.
- Epoxy-Coated Stamping Stacks — Stamped laminations individually coated with epoxy powder for superior insulation and corrosion resistance.
- Custom Stamping Stacks — Private mould development for unique slot counts, outer diameters, and tooth profiles.
Whether you need high-volume progressive die stamping or low-volume prototype stamping, Reenives can supply the right solution.
Key Specifications & Data
Below are typical specifications for Reenives rotor and stator stamping. Custom values are available upon request.
| Parameter | Typical Range / Value | Notes |
|---|---|---|
| Lamination Material | Silicon steel (e.g., 35WW250, 50WW470) | Low core loss grades |
| Lamination Thickness | 0.20 mm – 0.50 mm | Thinner = lower eddy current loss |
| Rotor Outer Diameter | 10 mm – 180 mm | Matched to stator bore |
| Stator Outer Diameter | 20 mm – 200 mm | Customizable |
| Stack Length | 5 mm – 80 mm | Affects torque & power |
| Slot / Pole Number | 6S/4P, 12S/14P, 24S/28P, etc. | Matched pairs |
| Stamping Method | High-speed progressive die | For high volume |
| Stamping Tolerance | ±0.05 mm (critical dimensions) | High-precision dies |
| Burr Height | ≤ 0.03 mm | Optimized die clearance |
| Insulation Coating | Epoxy powder coating | Uniform, pinhole-free |
| Core Loss (at 400Hz, 1T) | ≤ 25 W/kg | Material dependent |
| Die Life | 1–5 million strokes (typical) | Depends on material & maintenance |
Data source: Reenives internal testing & supplier material datasheets, 2024. Actual values may vary by design.
Applications of Rotor & Stator Stamping
Reenives rotor and stator stamping is used across a wide range of BLDC drone motor and brushless motor applications:
- FPV Racing Drones — High RPM, lightweight stamped stators and rotors with low cogging torque.
- Cinematic & Photography Drones — Smooth, vibration-free stamped cores for stable aerial footage.
- Agricultural Spraying Drones — Corrosion-resistant epoxy-coated stamped cores for harsh chemical environments.
- Industrial Inspection Drones — High-torque stamped cores for long endurance and heavy payloads.
- eVTOL & UAV Propulsion — Custom high-power stamped cores for next-generation air mobility.
- Robot Actuators — Low cogging torque stamped cores for precise motion control.
- EPS Motors — Low NVH stamped cores for automotive electric power steering systems.
- General BLDC Motors — Fans, pumps, power tools, and automotive actuators.

Reenives BLDC drone motor rotor and stator stamping powers FPV, agricultural, cinematic, and industrial UAVs worldwide.
How to Select the Right Rotor & Stator Stamping Process
Choosing the right rotor and stator stamping process for your BLDC drone motor involves several engineering and commercial decisions. Follow these steps:
- Determine Production Volume — High volume favors progressive die stamping; low volume or prototypes favor laser cutting or compound dies.
- Specify Lamination Material & Thickness — For high-RPM BLDC drone motors, use 0.20–0.25 mm low-loss silicon steel. For lower RPM, 0.35–0.50 mm is cost-effective.
- Define Critical Tolerances — Inner diameter, outer diameter, and slot dimensions typically require ±0.05 mm. Burr height should be ≤ 0.03 mm.
- Match Stator and Rotor — Ensure the stator bore and rotor outer diameter are designed as a matched pair with a controlled air gap (0.2–1.0 mm).
- Evaluate Die Design & Maintenance — Progressive dies with high-quality carbide inserts last longer and maintain precision. Ask about die maintenance schedules.
- Check Coating Capabilities — Epoxy powder coating for insulation and corrosion resistance. Ensure uniform, pinhole-free coverage.
- Request Sample Laminations — Test for burr height, dimensional accuracy, and magnetic performance before committing to production.
- Request Samples & Test — Reenives provides free samples for qualified projects. Test core loss, temperature rise, and mechanical fit.
FAQ — Rotor Stamping Parameters
Q1: What is the difference between progressive die stamping and compound die stamping for rotor and stator cores?
A: Progressive die stamping uses a multi-station die that performs cutting, notching, and forming operations sequentially as the coil feeds through. It offers the lowest cost per piece at high volumes and excellent consistency. Compound die stamping completes the entire lamination profile in a single press stroke, which is suitable for medium volumes and offers high precision with simpler tooling. For BLDC drone motor production above a few thousand pieces, progressive die stamping is usually more economical.
Source: Reenives engineering team, based on production experience.
Q2: What burr height can you achieve with your rotor and stator stamping process?
A: Our high-speed progressive die stamping process typically achieves a burr height of ≤ 0.03 mm with optimized die clearance and regular maintenance. This ensures clean stacking, reduces inter-lamination shorts, and minimizes vibration. Tighter burr control can be achieved for specific applications upon request.
Source: Reenives quality control standards, 2024.
Q3: What lamination thickness do you recommend for high-RPM BLDC drone motors?
A: For high-RPM BLDC drone motors (above 10,000 RPM), we recommend 0.20 mm or 0.25 mm silicon steel laminations for both rotor and stator. Thinner laminations significantly reduce eddy current losses, which helps keep the motor cool and improves efficiency. For lower RPM applications, 0.35 mm or 0.50 mm can be more cost-effective.
Source: Reenives engineering team, based on motor design guidelines and material datasheets.
Q4: What is the typical die life for progressive stamping of rotor and stator laminations?
A: Die life depends on the material grade, thickness, and maintenance schedule. For standard silicon steel (e.g., 35WW250) at 0.20–0.50 mm thickness, a high-quality carbide progressive die typically achieves 1–5 million strokes before major refurbishment. Regular maintenance and sharpening extend die life and maintain precision.
Source: Reenives tooling engineering data, 2024.
Q5: Why must the rotor and stator be designed as a matched pair?
A: The stator and rotor form a single magnetic circuit. If they are not matched — wrong air gap, mismatched pole/slot count, or different thermal expansion — the motor can suffer from high cogging torque, reduced efficiency, vibration, and premature bearing wear. Buying a matched rotor-stator pair from a single supplier ensures the air gap, tolerances, and magnetic design are optimized together. Our high-precision stamping ensures stator bore and rotor outer diameter tolerances of ±0.05 mm, allowing reliable small air gaps.
Source: Reenives engineering team, based on motor design principles.
Q6: Can you develop custom rotor and stator stamping for my specific BLDC drone motor?
A: Absolutely. We support private mould development. Provide us with your required stator outer diameter, stator bore, rotor outer diameter, stack length, slot/pole combination, and magnet configuration. Our R&D team will design and produce custom stamping dies and matched stator/rotor cores tailored to your motor. Tooling lead time is typically 15–25 days.
Source: Reenives custom development process.
Summary — Get Your Rotor Stamping Quote Today
Ready to Improve Your BLDC Drone Motor Performance with Precision Stator & Rotor Stamping?
Reenives is a reliable BLDC drone motor stator rotor stamping supplier with 4 years of manufacturing experience, 100+ R&D patents, and 3 production bases. We serve 1000+ enterprises worldwide with high-precision rotor and stator stamping for UAV and BLDC motors.
📦 Bulk purchasing · 🔧 Private mould development · 🧪 Free samples
🌐 Official Website: www.reenives-bldcmotor.com
📧 Email: linda_reenives@163.com
Contact us now for a free sample and tailored solution for your production scenario.
Dongguan Runlu Motor Technology Co., Ltd.
Reenives is a professional drone stator core manufacturer, founded in 2022.
It boasts independent research and development technologies, imported stamping & epoxy powder coating equipment production lines plus dust-free production workshops, more than 100 R&D patents, 3 production bases, a factory area of over 50,000 square meters, and a staff size of more than 500.
From production to sales, we support bulk purchasing, private mould develop, and samples making, and can provide tailor-made perfect solutions for your production and usage scenarios. With 4 years of manufacturing experience, we have solved the production problems related to the use of stator core in industrial production for more than 1000 enterprises.
We can ship globally (with complete export qualifications). Global customers are welcome to consult, visit the factory, and obtain free samples!
Reenives Runlu Motor Rotor Stamping
Related Article