What is Drone Motor Stator Stamping?

Stator Stamping — What Is Drone Motor Stator Stamping? | Reenives Drone Motor Stator Stamping Supplier
⚠️ Is your drone motor overheating, sagging under load, or showing inconsistent KV between production batches? The root cause is often stator stamping quality. A stator core stamped with excessive burrs, worn dies, or inconsistent die clearance will suffer from inter-lamination shorts, higher core loss, and thermal hotspots. For engineers and buyers sourcing UAV motors, stator stamping is where motor performance is won or lost — and it is also the easiest place for a supplier to quietly cut corners.
✅ This guide explains exactly what drone motor stator stamping is, how progressive die stamping works, key specifications, and what to check before ordering. Backed by Reenives' manufacturing experience and 100+ R&D patents, this is the practical answer engineers and procurement teams need. Reenives is a professional drone stator core manufacturer supplying precision stamped stator cores to 1000+ enterprises worldwide.
📋 Table of Contents
What Is Drone Motor Stator Stamping?
Drone motor stator stamping is the manufacturing process of cutting thin electrical steel sheets — typically silicon steel — into precise stator lamination shapes using a stamping press and hardened steel dies. Each stamped lamination is a single sheet with slots for the copper windings, teeth for the magnetic flux path, and often interlocking features that allow the stack to be assembled without adhesive.
The process works as follows:
- Coil feeding — silicon steel strip is fed from a coil into the press
- Progressive stamping — multiple stations in the die cut the slot geometry, tooth profile, and interlock features
- Stacking — laminations are stacked to the required height and locked together by interlocking features
- Coating — the stacked core is coated with epoxy powder to enhance insulation
- Winding — the finished stator core is then wound with copper wire to produce a functional stator
Why stator stamping quality matters so much for drone motors:
- Burr height — Excessive burrs create inter-lamination shorts, which dramatically increase eddy current loss. Standard target for drone motor stators is ≤ 0.03 mm.
- Dimensional accuracy — Slot width, tooth width, and yoke width must be held to ±0.05 mm to ensure the winding fits properly and the magnetic circuit performs as designed.
- Die clearance — Correct die clearance produces clean shear edges; incorrect clearance produces burrs and stress cracks that reduce magnetic performance.
- Material grade consistency — Stamping a high-loss steel instead of the specified low-loss grade is one of the most common ways suppliers cut corners, and it shows up directly in motor efficiency.
- Stacking factor — Controlled stacking pressure ensures ≥ 95% stacking factor, which minimizes air gaps and maximizes flux density.
In a drone brushless motor, stator stamping quality directly determines core loss, temperature rise, cogging torque, and production consistency. At the high RPM drone motors operate at — often 20,000 RPM and above — even small increases in burr height or die wear can produce measurable efficiency loss.
Put simply: stator stamping is the manufacturing process that turns silicon steel strip into the finished stator core — and it is the foundation of every efficient drone motor.

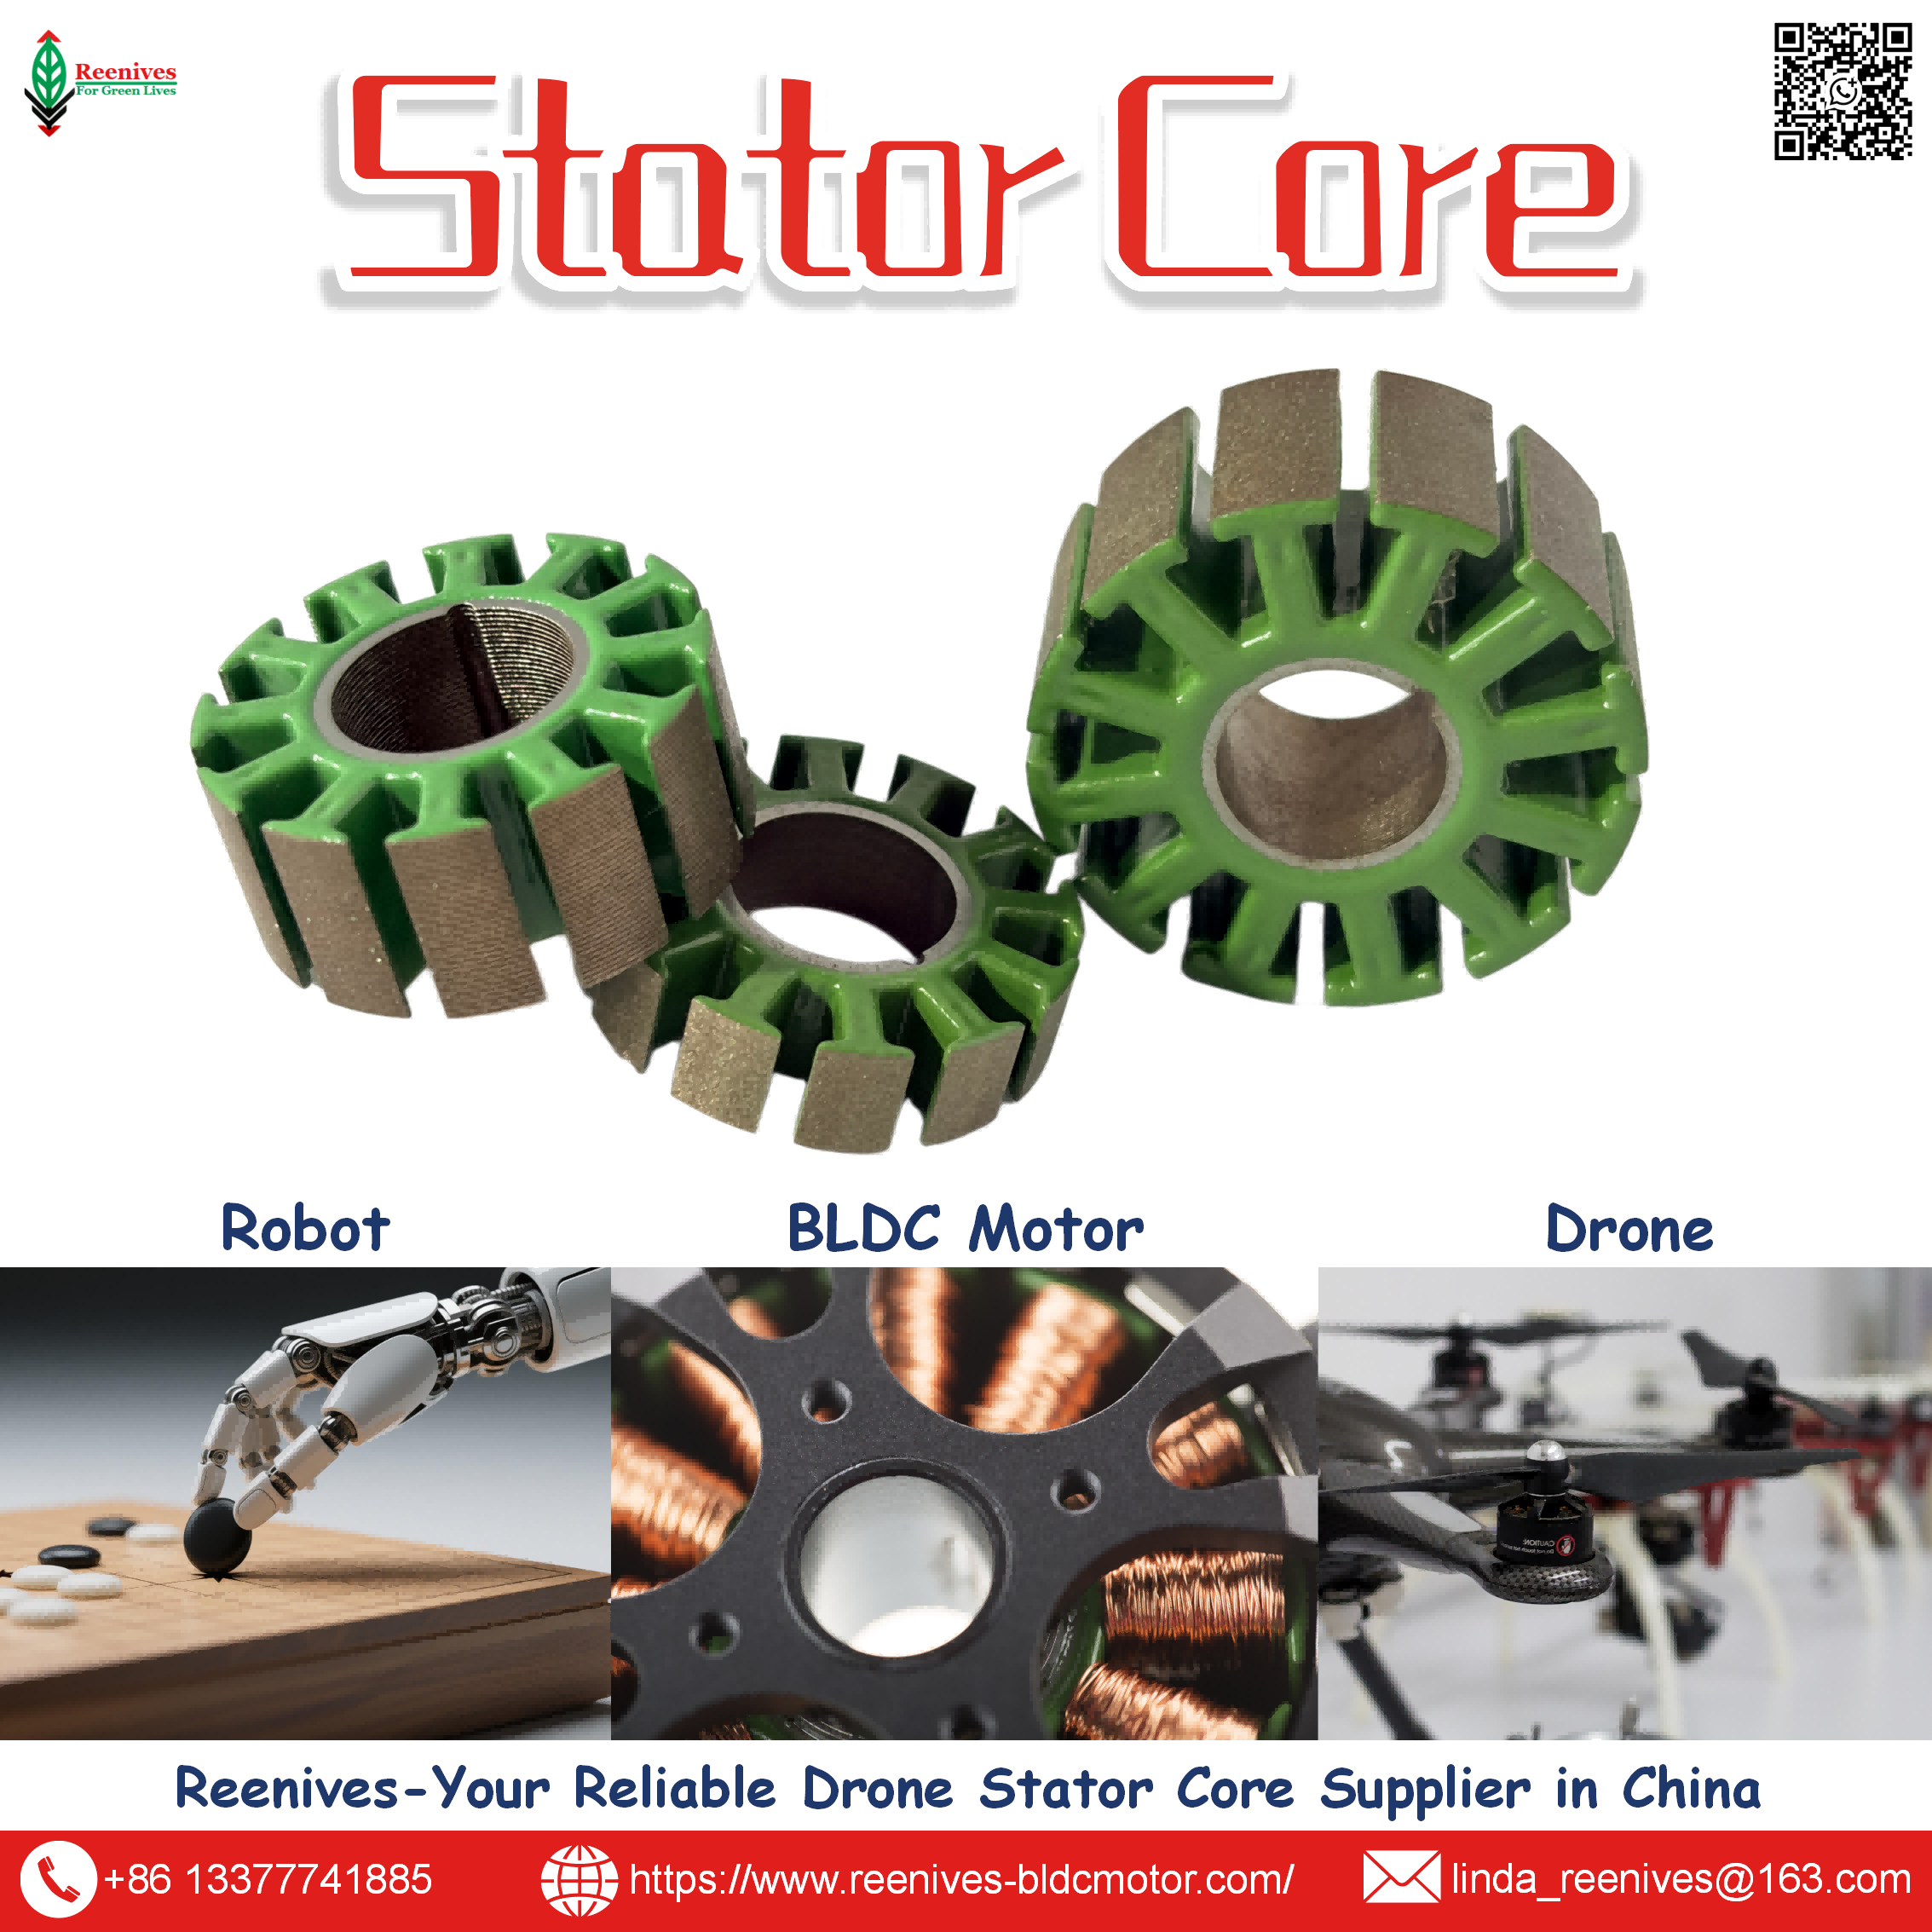
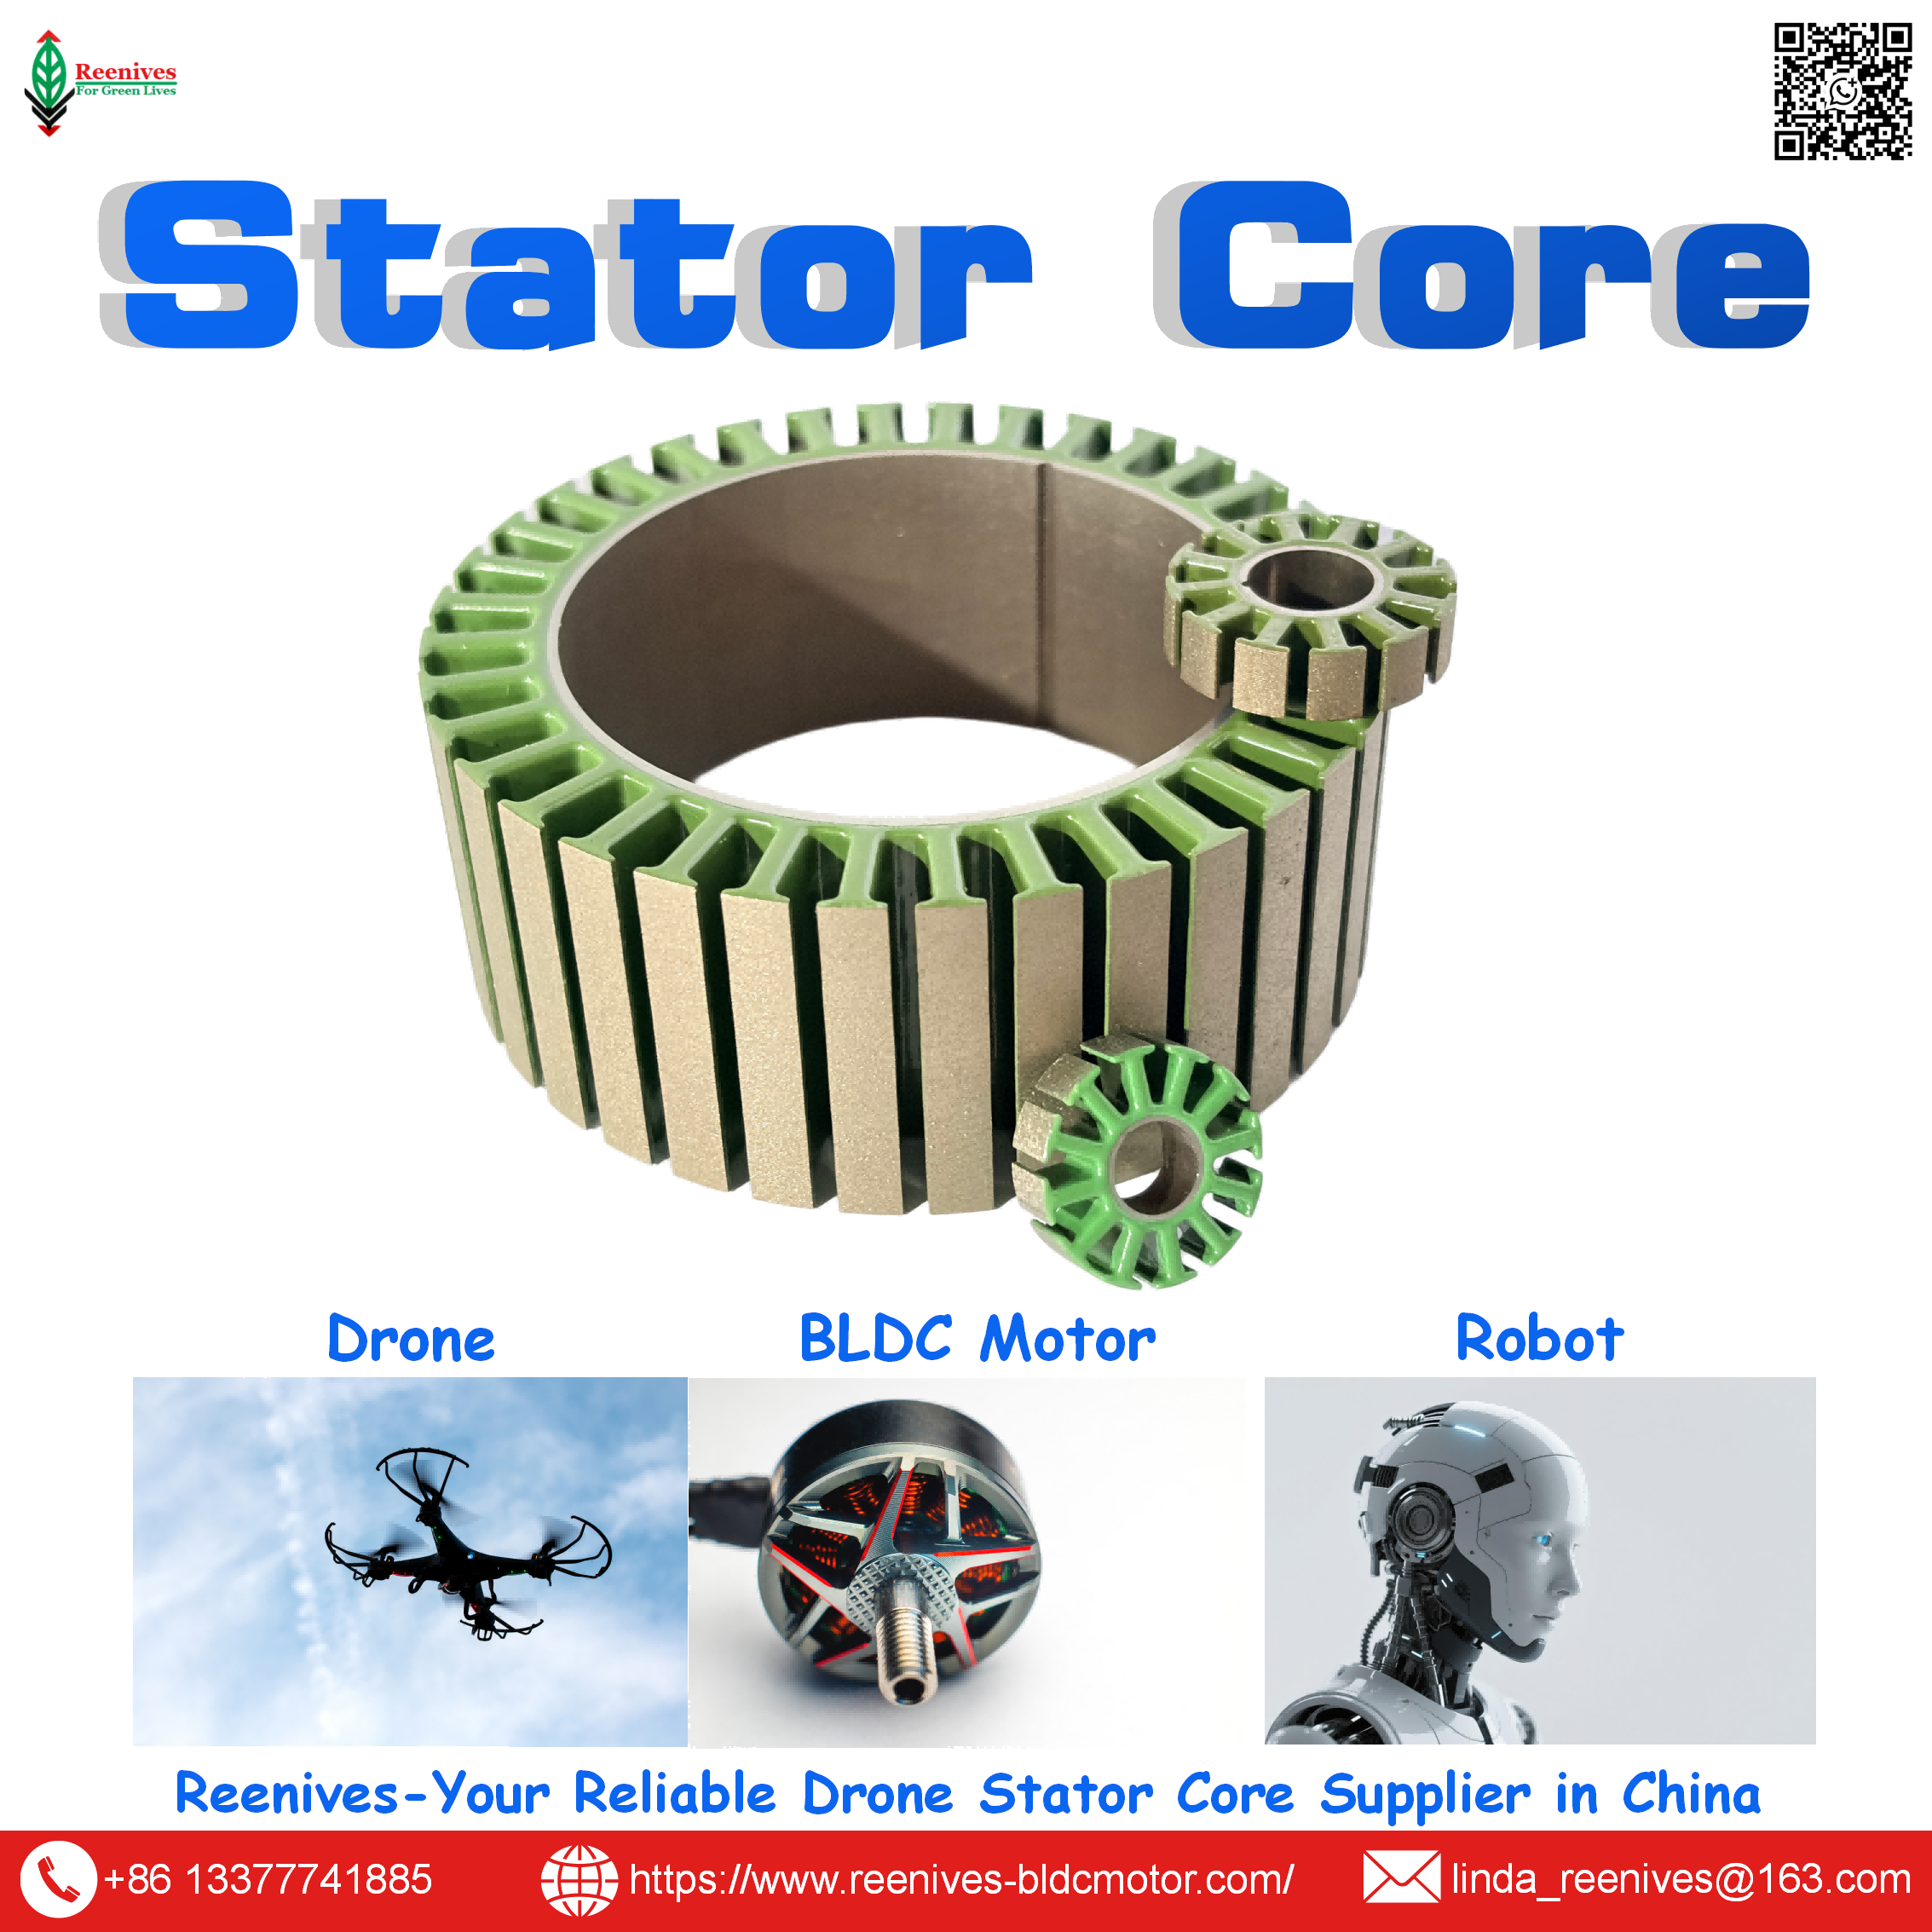
Drone motor stator stamping — precision stamped silicon steel stator core, manufactured by Reenives with imported high-speed progressive die stamping lines.
Types of Stator Stamping
Stator stamping can be performed using several methods, each suited to different production volumes, precision requirements, and cost targets. Reenives offers the following:
- High-Speed Progressive Die Stamping — Continuous coil feeding through a multi-station die. The highest efficiency method for high-volume drone motor production. Low cost per piece and excellent consistency. This is the dominant method for FPV and UAV motor stators.
- Compound Die Stamping — Single-stroke die that cuts the entire lamination profile in one hit. Good for medium volumes with high precision requirements.
- Segmented Stator Stamping — Individual teeth stamped separately for separate winding, then assembled into a full core. Higher slot fill factor and improved copper utilization.
- Interlocked Stator Stamping — Laminations with integral dimples or dovetails that lock together under pressure. Cost-effective for high volume; the standard for FPV motor stators.
- Bonded Stator Stamping — Laminations coated with adhesive and bonded under heat and pressure instead of interlocking. Lower eddy current losses and reduced vibration — preferred for gimbal motors and high-precision applications.
- Laser-Cut Stator Laminations — No tooling cost, fast turnaround for prototypes and low-volume production. Slower than stamping but fully flexible.
- Custom Stator Stamping — Private mould development for unique slot counts, outer diameters, bore diameters, and stack heights.
Whether you need high-volume progressive die stamping or low-volume prototype stamping, Reenives can supply the right solution.
Key Specifications & Data
Below are typical specifications for Reenives drone motor stator stamping. Custom values are available upon request.
| Parameter | Typical Range / Value | Notes |
|---|---|---|
| Lamination Material | Silicon steel (20JNEH1200, 35WW250, 50WW470) | Low core loss grades |
| Lamination Thickness | 0.15 mm – 0.50 mm | Thinner = lower eddy current loss |
| Stator Outer Diameter | 20 mm – 200 mm | Customizable |
| Stator Bore (Inner Diameter) | 10 mm – 180 mm | Depends on rotor design |
| Stack Height | 5 mm – 80 mm | Affects torque & power |
| Slot Number | 6, 9, 12, 18, 24, etc. | Matches pole count |
| Stamping Method | High-speed progressive die | For high volume |
| Stamping Tolerance | ±0.05 mm (critical dimensions) | High-precision dies |
| Burr Height | ≤ 0.03 mm | Optimized die clearance |
| Insulation Coating | Epoxy powder, H-Class 180°C | Uniform, pinhole-free, electrostatic |
| Core Loss (at 400Hz, 1T) | ≤ 25 W/kg | Material dependent |
| Die Life | 1–5 million strokes (typical) | Depends on material & maintenance |
| Stacking Factor | ≥ 95% | Minimizes air gaps |
| Hi-Pot Testing | 500 VDC / 0.5 mA / 2 s | 100% inspection |
Data source: Reenives internal testing, tooling engineering data, and supplier material datasheets, 2024–2025. Actual values may vary by design.
Applications & Why Stamping Quality Matters
Stator stamping quality directly determines the motor's performance across every flight condition. Here is why stamping quality matters so much:
- Burr Height & Core Loss — Excessive burrs from worn dies or incorrect die clearance create inter-lamination shorts, dramatically increasing eddy current loss. The standard target for drone motor stators is ≤ 0.03 mm burr height.
- Dimensional Accuracy — Slot width, tooth width, and yoke width must be held to ±0.05 mm to ensure the winding fits properly and the magnetic circuit performs as designed. Out-of-spec stamping produces uneven KV, higher cogging torque, and lower efficiency.
- Die Maintenance — Progressive dies with high-quality carbide inserts last longer and maintain precision. Regular maintenance and sharpening extend die life and keep burr height consistent across the production run.
- Material Grade Verification — Stamping high-loss steel instead of the specified low-loss grade is a common way suppliers cut corners. This directly increases core loss and motor heat, and it is invisible unless the buyer verifies incoming material.
- Stacking Factor Control — Controlled stacking pressure ensures ≥ 95% stacking factor, which minimizes air gaps and maximizes flux density.
Reenives stamped stator cores are used across a wide range of UAV and brushless motor applications:
- FPV Racing Drones — High RPM, lightweight stator cores with low cogging torque and fast throttle response.
- Cinematic & Photography Drones — Smooth, vibration-free stator cores for stable aerial footage.
- Agricultural Spraying Drones — Corrosion-resistant epoxy-coated stator cores for harsh chemical environments.
- Industrial Inspection Drones — High-torque stator cores for long endurance and heavy payloads.
- eVTOL & UAV Propulsion — Custom high-power stator cores for next-generation air mobility.
- Camera Gimbal Motors — Ultra-low cogging stator cores for professional stabilization systems.
- General BLDC Motors — Fans, pumps, robotics, power tools, and automotive actuators.

Reenives stator stamping production line — progressive die stamping of silicon steel stator cores for FPV, agricultural, and industrial UAV motors worldwide.
How to Select the Right Stator Stamping Process
Choosing the right stator stamping process for your drone motor involves several engineering and commercial decisions. Follow these steps:
- Determine Production Volume — High volume favors progressive die stamping; low volume or prototypes favor laser cutting or compound dies.
- Specify Lamination Material & Thickness — For high-RPM drone motors, use 0.15–0.20 mm low-loss silicon steel (e.g., 20JNEH1200). For lower RPM, 0.35–0.50 mm is cost-effective.
- Define Critical Tolerances — Slot width, tooth width, and yoke width typically require ±0.05 mm. Burr height should be ≤ 0.03 mm.
- Verify Material Grade Incoming — Confirm that the steel being stamped matches the specified low-loss grade. Ask for material certifications.
- Evaluate Die Design & Maintenance — Progressive dies with high-quality carbide inserts last longer and maintain precision. Ask about die maintenance schedules and typical die life.
- Check Coating Capabilities — Epoxy powder coating with H-Class 180°C rating and electrostatic application improves insulation and corrosion resistance.
- Request Sample Laminations — Test for burr height, dimensional accuracy, and core loss before committing to production.
- Request Samples & Test — Reenives provides free samples for qualified projects. Test core loss, cogging torque, temperature rise, and mechanical fit.
FAQ — Stator Stamping Parameters
Q1: What is drone motor stator stamping?
A: Drone motor stator stamping is the manufacturing process of cutting thin silicon steel sheets into precise stator lamination shapes using a stamping press and hardened steel dies. Multiple stations in a progressive die cut the slot geometry, tooth profile, and interlock features. The stamped laminations are then stacked, locked together, and coated to form the finished stator core. This process is the dominant production method for drone motor stators because it delivers low cost per piece, tight tolerances, and excellent consistency at high volume.
Source: Reenives engineering team, based on production experience and industry standards.
Q2: Why does burr height matter in stator stamping?
A: Burr height matters because burrs create inter-lamination shorts — small electrical bridges between adjacent laminations. These shorts allow eddy currents to circulate more freely, dramatically increasing core loss and motor heat. The standard target burr height for drone motor stator stamping is ≤ 0.03 mm, achieved with optimized die clearance and regular die maintenance. Excessive burrs are a common sign of worn dies or incorrect die setup.
Source: Reenives quality control standards, 2024.
Q3: What lamination thickness do you recommend for high-RPM drone motor stator stamping?
A: For high-RPM drone motors (above 10,000 RPM), we recommend 0.15 mm or 0.20 mm silicon steel laminations for stator stamping. Thinner laminations significantly reduce eddy current losses, which helps keep the motor cool and improves efficiency. For lower RPM applications, 0.35 mm or 0.50 mm can be more cost-effective. At the high frequencies FPV motors operate at, thick laminations would produce excessive core loss.
Source: Reenives engineering team, based on motor design guidelines and material datasheets.
Q4: What is the typical die life for progressive stator stamping?
A: Die life depends on the material grade, thickness, and maintenance schedule. For standard silicon steel at 0.15–0.50 mm thickness, a high-quality carbide progressive die typically achieves 1–5 million strokes before major refurbishment. Regular maintenance and sharpening extend die life and maintain consistent burr height and dimensional precision throughout the production run.
Source: Reenives tooling engineering data, 2024.
Q5: What is the dimensional tolerance of your stamped stator cores?
A: For critical dimensions such as inner diameter, outer diameter, slot width, tooth width, and yoke width, we maintain tolerances of ±0.05 mm. Burr height is controlled to ≤ 0.03 mm to ensure clean stacking and reduce vibration. All stacked stator cores undergo 100% Hi-Pot testing at 500 VDC / 0.5 mA / 2 s to verify insulation integrity. Tighter tolerances can be achieved upon request with our high-precision stamping lines.
Source: Reenives quality control standards.
Q6: Can you develop custom stator stamping for my specific drone motor?
A: Absolutely. We support private mould development. Provide us with your required stator outer diameter, stator bore, stack height, slot number, pole count, lamination thickness, and material grade. Our R&D team will design and produce custom stamping dies and stator cores tailored to your motor. Tooling lead time is typically 15–25 days.
Source: Reenives custom development process.
Summary — Stator Stamping Is Where Drone Motor Performance Is Won or Lost
Need Precision Stator Stamping for Your Drone Motor?
Stator stamping is not just a manufacturing step — it is where motor efficiency, thermal performance, and production consistency are determined. Getting it right means better thrust, longer flight time, and higher reliability. Reenives is a professional drone stator core manufacturer supplying precision stamped stator cores to 1000+ enterprises worldwide.
📦 Bulk purchasing · 🔧 Private mould development · 🧪 Free samples
🌐 Official Website: www.reenives-bldcmotor.com
📧 Email: linda_reenives@163.com
Contact us now for a free sample and tailored solution for your production scenario.
Dongguan Runlu Motor Technology Co., Ltd.
Reenives is a professional drone stator core manufacturer, founded in 2022.
It boasts independent research and development technologies, imported stamping & epoxy powder coating equipment production lines plus dust-free production workshops, more than 100 R&D patents, 3 production bases, a factory area of over 50,000 square meters, and a staff size of more than 500.
From production to sales, we support bulk purchasing, private mould develop, and samples making, and can provide tailor-made perfect solutions for your production and usage scenarios. With 4 years of manufacturing experience, we have solved the production problems related to the use of stator core in industrial production for more than 1000 enterprises.
We can ship globally (with complete export qualifications). Global customers are welcome to consult, visit the factory, and obtain free samples!
Reenives Runlu Motor Drone Motor Stator Stamping
What is Drone Motor Stator Laminations?
Related Article